Fiber Laser Metal Marking for UK Workshops
A desktop CO₂ laser will not mark bare stainless in a way that survives handling. At 10.6μm the beam reflects off bare metal instead of being absorbed, so more power and more passes do not rescue it. That is a machine-class limit, not a settings problem.
Fiber lasers run at 1064nm, where metal absorbs energy. That is the class of machine used for annealing, etching, and deep marking on stainless, aluminium, brass, and coated surfaces. If you are comparing the fiber laser range on OMTech UK, the decision is less about wattage and more about which mark you are selling — a grey etch, a black anneal, or a colour mark that comes straight off the beam. This guide is for the UK workshop making that decision, and for anyone bringing a machine into a shared space who needs to understand the safety and compliance layer before the first paid job.

Class 4 in the UK — the short version
These are Class 4 laser products. BS EN 60825-1 is the laser safety standard that applies in the UK, and the Health and Safety Executive (HSE) expects a risk assessment, adequate ventilation, safety signage, and maintenance records if the machine is used commercially or in a shared workshop. In practice: wavelength-matched eyewear, an enclosure or interlock that actually works, and fume extraction for coated or plated metals. The UK small business guide covers COSHH, insurance, and PAT testing alongside the laser-specific requirements. If you are importing a machine from outside the UK, VAT at 20% applies to the landed value, and the courier’s handling fee is a separate line.
What the Fiber Beam Does to Metal
Three marks come out of the same machine, and the difference is heat input and pulse control, not wattage alone. The fibre laser technology guide on OMTech UK explains the wavelength and beam-delivery difference if you are still separating fibre marking from fibre cutting.
Annealing
The surface heats without melting and grows a dark oxide layer. That is how a serial number goes onto a stainless instrument, a tool tag, or a firearm part without removing material. The mark is a chemical change, not a coating sitting on top of the metal, so it does not rub off in normal handling.
How long it survives is a separate question. On stainless that will see moisture, salt, or cleaning chemicals — an outdoor part that goes through British weather and road salt — the alloy and the heat input decide whether the marked area stays corrosion-resistant. Test the exact alloy and leave it for a few weeks before promising a service life to a customer.
Etching
A thin surface layer vaporizes. High contrast, shallow, fast. The default for logos and names on tools, tags, and small parts where speed matters more than depth.
Deep Engraving
Material is removed over multiple passes. Rated maximum marking depth is roughly 0.04mm on a 20W fiber, 0.1mm on a 50W fiber or 60W MOPA, and 0.13mm on an 80W MOPA. Treat those as ceiling figures under specific lens and material conditions, not a guarantee on every job. Depth accumulates through multiple fast hatch passes, not one slow heavy pass at 100% power. If you are running a single pass at full power and wondering why the surface looks burnt instead of deep, that is the misunderstanding. And if 0.5mm-plus is a real requirement, you are in a different machine class than a marking laser.
What Each Metal Gives You
| Metal | What you get | UK shop context |
|---|---|---|
| Stainless steel | Black annealed mark or white etch | Serialized parts, drinkware, industrial nameplates, tool tags. Colour marking on stainless needs MOPA; a standard fiber is largely grayscale. |
| Carbon steel | Dark, high-contrast etch | Fast and forgiving for tags, tool marking, and agricultural equipment labels. |
| Anodised aluminium | White metal revealed under the coating | Cleanest-looking result on the list; common on promotional products, outdoor gear, and corporate awards. |
| Bare aluminium | Light gray mark | Works, but lower contrast — test before quoting a production run. |
| Brass | Golden, deep-contrast mark | Badges, plaques, and gift-shop hardware. |
| Copper | Dark, crisp mark | Lower absorption than steel; MOPA gives more consistent results than standard fiber. |
| Coated metals | Coating burned away, base metal exposed | Powder-coated drinkware and painted panels — the same gift-shop product in a different machine class. |
Silver and gold absorb 1064nm less efficiently than the metals above, so precious-metal jewellery work needs different expectations than steel, brass, or aluminium.

Standard Fiber, MOPA, or Galvo
These three words get used interchangeably and cause bad purchases. They are not the same axis.
Standard Fiber (Q-switched)
Fixed pulse characteristics, marks the common metals well, and is the cheapest way into fiber. A 50W unit with a roughly 200×200 mm work area is a typical first machine. Frequency range is narrow by MOPA standards (around 20–100 kHz), and colour marking on stainless is limited to grayscale. For names, logos, serial numbers, and industrial tags, this class covers the work.
MOPA
Pulse width and frequency are independently adjustable, and that is the entire point. A MOPA source can go from 2 ns pulses for fine, low-heat detail to 200 ns and beyond for deep black annealing, with frequency from 1 kHz to 4000 kHz. That combination is what produces colour marking on stainless and clean marks on anodised aluminium.
If laser colour marking — colour straight off the beam, nothing added afterwards — is a product you want to sell, MOPA is the requirement, not the upgrade. A 60W MOPA is the volume workhorse; 100W is available when per-pass headroom becomes the bottleneck. But if the work mix is mostly paint fill, serial numbers, and logos, a standard 20–50W fiber covers it without the MOPA premium.
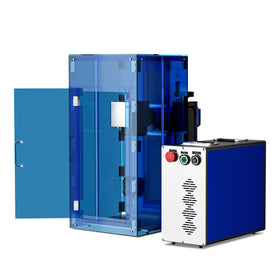
Galvo is not a laser type. It is the beam-steering mechanism — mirrors move the beam instead of a gantry moving a head, which is why these machines are rated to 7,000–10,000 mm/s. Nearly every compact fiber and MOPA machine is galvo-based. Split versus integrated is a floor-space and enclosure decision, not a marking-quality decision. If you want to compare the body styles side by side, the MOPA and fiber laser collection lists both.
What Wattage Actually Buys You
20W
≈0.04mm depth
Light marking, coated metals, anodised aluminium
50W
≈0.1mm depth
General metal marking, production speed
60W MOPA
≈0.1mm depth
Colour marking plus depth, higher throughput
80W MOPA
≈0.13mm depth
Deeper marks within lens limits, high-volume work
Extra watts buy speed and headroom, not unlimited depth. A 30W and a 60W land in the same depth class. Percentage power is also machine-relative: 30% on a 60W is twice the absolute energy of 30% on a 30W, so settings do not transfer between models. Anyone quoting “30% power, 400 mm/s” without naming the machine is handing you half a recipe.
Software Settings That Decide the Result
Hardware gets you the beam. Software decides whether the mark looks professional. OMTech MOPA machines ship with EzCad2, and the same hardware runs LightBurn’s galvo version; both expose the same handful of controls. The laser basics guides cover the parameter relationship if you want a reference rather than a single recipe.
Fill, Line Interval, and Loop Count
- Hatch (fill) turns an outline into a solid mark. Metal engraving is a fill operation, not an outline operation.
- Line interval is the spacing between hatch lines. Fine detail and smooth surfaces want 0.01–0.05mm. Too wide and you see stripes; too tight adds heat and time without adding darkness.
- Loop count is how many times the fill repeats. Depth comes from loops, not from maxing power. Two or three loops at moderate power beat one blast at 100%, and they do not cook the surrounding metal.
Hatch Angle
Rotate the hatch angle between passes — classically 45°, 90°, 135°. Stacking passes at the same angle leaves a brushed, directional texture that catches light badly. Crossing the angles evens out the surface. This one setting separates deep engraving from a surface that looks like someone dragged a comb across it.
Focus
Fiber focus is set with the dual red dots — two beams converge into a single point at the correct focal distance — or with the supplied focus ruler. You cannot eyeball this the way you might on a CO₂ bed. The focal spot is tiny, and a millimetre off visibly reduces contrast. Re-check whenever the machine moves or the workpiece height changes. In a shared UK workshop — a makerspace, a rented unit, a garage that doubles as a business — “the machine moved” happens more often than people admit.
 Settings to Test First
These are starting points for OMTech fiber and MOPA machines only. Do not copy them to another brand without re-testing, and do not port them from a CO₂ tutorial. The wavelength is different, and so is the absorption behaviour. For stainless-specific starting points, the stainless steel settings guide breaks dark annealing and deep engraving into separate parameter sets.
| Parameter | Starting point | What it changes |
|---|---|---|
| Power | 20–40% | Darkness and heat input; on MOPA, colour depends on keeping this low and stable. |
| Speed | 300–1500 mm/s | Higher speed gives a lighter mark; fiber tolerates far higher speeds than CO₂. |
| Frequency | 1–4000 kHz (MOPA); 20–100 kHz for standard fiber | Higher frequency is smoother and lighter; lower is deeper and rougher. Standard fiber and MOPA do not share the same frequency window. |
| Pulse width | 2–500 ns on MOPA; fixed around 80–140 ns on standard fiber | Short pulses for fine detail and colour; long pulses for deep black. Standard fiber has no independent pulse-width control. |
| Line interval | 0.01–0.05 mm | Stripe visibility versus heat build-up. |
| Loop count | 1–3 | Depth; add loops instead of power. |
| Hatch angle | Rotate 45° per pass | Eliminates directional brushing. |
Five Mistakes That Ruin Metal Jobs
Where the Money Is in the UK
The fiber applications that pay for themselves fastest in the UK market are serialised tool and equipment tags, industrial nameplates and UID plates on recurring contracts, powder-coated drinkware, challenge coins and award pieces with paint fill, and brass or steel branding for pubs, cafés, and trade businesses. Most are repeat orders rather than one-offs, which is what makes the machine economics work in a market where premises costs and electricity tariffs punish idle equipment.
Two different techniques get called “colour” in this trade, and mixing them up is how people buy a machine they do not need.
Paint Fill
Engraving a recess, rubbing enamel or paint into it, then wiping the surface clean so only the recessed area stays filled. The laser cuts the pocket; the colour comes out of a jar. A standard fiber does this perfectly well. Challenge coins, filled badges, and most signage-style work are paint fill.
Laser Colour Marking
The beam itself grows a thin oxide film whose thickness produces the colour, with nothing added afterwards. That needs the pulse control of a MOPA source. If a customer wants a red or blue mark straight off the bed — no paint, no fill — that is the requirement, and a standard fiber cannot deliver it.
So the mapping is: serial numbers, logos, plaques, nameplates, and paint-filled work all run on a 20–50W standard fiber. Add MOPA money only for unpainted colour marking, or for delicate thin-material work where the short-pulse range matters. If the mix is mostly the first list, do not pay for the second.
On the business side, the UK VAT registration threshold is £90,000 turnover in a rolling 12-month period. Below that, registering is optional; above it, it is mandatory, and the 20% VAT applies to the goods and services you sell. That is a separate line from the machine purchase, but it belongs in the same spreadsheet when you are working out whether the fiber laser pays for itself in the first year or the second.

Frequently Asked Questions
Can a CO₂ laser mark metal instead?
On a desktop CO₂ machine, only with a coating spray that creates an absorptive layer. It works for occasional experiments, but contrast and durability are worse, and you are buying consumables forever. Industrial CO₂ equipment with assist gas is a different class of machine and a different budget. If metal is more than an experiment, a fiber source is the machine class built for it.
Is the fiber mark permanent?
It does not wash off or rub away in normal handling, because it is a change to the surface rather than ink sitting on top. It is not indestructible. An annealed mark’s corrosion resistance depends on the alloy and the heat input, and a deep etch can hold moisture in a way a polished surface does not. For parts that see road salt, cleaning chemicals, or abrasion, test the actual alloy before promising a service life.
Will a fiber laser cut metal?
Not thick stock. Cutting is a separate machine class. Marking-class fiber lasers engrave, anneal, and etch. A 2000W-class source is a cutter; a 20–100W marking fiber is not. The fibre laser technology guide explains the wavelength and power gap in plain terms.
What laser safety standard applies in the UK?
BS EN 60825-1 is the laser safety standard for equipment in the UK, and the HSE expects a risk assessment, ventilation, signage, and maintenance records for commercial use. Class 4 operation requires wavelength-matched eyewear, an enclosure or interlock, and fume extraction. The machine’s CE/UKCA marking is the starting point, not the whole story — the workspace and the operator’s PPE are the shop’s responsibility.
Before quoting anyone
Test the alloy. Then trust the mark.
Start with one plate of the stainless you actually sell. Run three passes with hatch angles at 45°, 90°, and 135°, all at the same power and loop count, then compare the three marks under normal room light. You will see the brushed texture disappear, and you will know what the machine can do before a UK customer sees a quote.
Compare MOPA and fiber lasers →The fiber laser range on OMTech UK runs from 20W standard fiber up to 100W MOPA. Start from the wattage that matches the jobs you can name — and if the machine is going into a shared workshop, sort the eyewear, the interlock, and the fume extraction before the first paid job, not after.